







Advertising [Product3rdColumn]
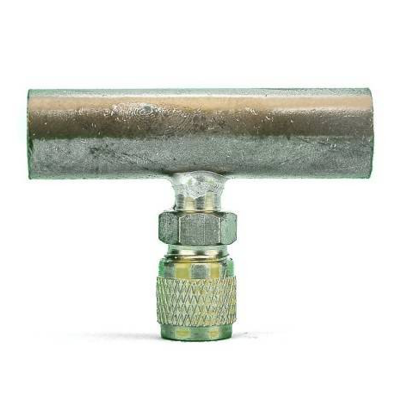
Copper coupling 3/4 solder union with Obus valve cap
Copper hose for refrigerant gas charging - with cap and valve. - Size: 3/4" X 3/4"
IMPORTANTE: No se aceptan devoluciones de compresores ni unidades condensadoras. Asegúrese que producto necesita antes de realizar su compra.
Types of torch welding: soft and hard solderingIn this article you will see everything you need to know to perform welding of copper pipes or other metals using a torch, very useful if you want to repair a copper pipe leak or if you want to install a radiator, a sink, etc. Welding copper or other metals with a torch consists of joining copper parts with the help of a second metal that melts between them. The melting temperature of the filler metal rod must be lower than that of the copper or metal to be welded. The part to be welded does not melt, therefore it is not a fusion welding of the base material. This type of welding is used when you want to join different materials, or those that have poor weldability and high strength is not required. It is the easiest welding technique to perform, even for DIY beginners.There are two types of welding with regard to the melting temperature of the filler material: soft soldering and hard soldering. Soft soldering requires reaching temperatures below 450ºC, while hard soldering uses temperatures above 450ºC. For example, filler materials made of silver and copper require temperatures of 600ºC and 900ºC. The higher the melting temperature of the filler material, the greater the strength of the joint. In electronics, the filler material consists of 60% tin and 40% lead and the temperature required for its melting is only 190ºC. Previously with lead pipes, a large proportion of lead was used in the filler material, but nowadays with copper pipes it has been removed from the filler material and replaced with copper and a higher proportion of tin. The filler material used in hard soldering is generally an alloy of copper, copper phosphate and zinc, or copper and silver. The melting point is between 600ºC and 880ºC. Alloys with a high proportion of silver (40%) are recommended for performing welds with high mechanical strength and are those used for joints of copper and brass gas pipes. Brass is used for joining steel parts. The filler metal or flux is used with a flux, which is responsible for removing impurities from the joint surface and also oxides so that the flux adheres well.Choosing the right torch depending on the type of welding to be performedThe soldering lamp: is powered by a butane or butane/propane cartridge. It is ideal for performing soft soldering (with tin wire). Soldering torch: is powered by butane or propane gas cylinders and provides a larger flame, usually come with various nozzles for different applications. This torch is used to weld different metals and alloys: tin, copper, brass, aluminum and zinc. Its use is not recommended for ferrous metals as it offers little mechanical strength in joints. Bi-gas torch: is powered by an LPG or acetylene cartridge, mixed with oxygen under pressure, coming from another tank. It is ideal for performing hard soldering of large diameter pipes and also for ferrous metals. Professionals usually use this type of torch for all hard soldering as it greatly facilitates their work by providing higher temperature. Choice of filler metal or flux The choice of filler metal will depend on the type of material to be welded and the strength required for the joint and will influence the type of torch to be used. The more resistant the filler material, the higher its melting temperature. Type of welding Mechanical strength Application Soft soldering (tin) Weak: 5 kg/mm2 Installation of fixtures, extension of water lines. Hard soldering (copper/phosphorus) 50 kg/mm2 Cold and hot water pipes, radiators, water circuits. Copper/silver 6% and 20% 60 kg/mm2 Facilitates professionals in achieving strong and watertight joints. The silver content helps rotate the parts while they are being welded ensuring good sealing. Copper/silver 40% 40 kg/mm2 Copper pipe for gas. Procedure for welding with a torch The material to be welded must be prepared very well, sanding the two surfaces to be joined with sandpaper. Then, with a soft cloth we remove the dust and finally with a brush. We apply the flux to the joint that will receive the filler metal and fit the pieces in their final place. The pieces to be welded must be held (if necessary) with clamps since copper and its alloys are good heat conductors. If you are going to weld against a wall, there are special fire-resistant fabrics to isolate the wall from the torch flame. As we have seen for home DIY, the torch
feedback Report comment